Agricultural cooperatives face a major operational bottleneck during harvest season. Decentralized, outdated milling equipment causes severe processing inefficiency, demands high manual labor input, and produces unacceptable grain breakage rates. Cooperatives must balance strict capital constraints with the necessity for commercial-grade output. High head rice yields and low broken grains are mandatory to compete in premium agricultural markets. Buyers reject shipments with excessive broken kernels or poor polishing.
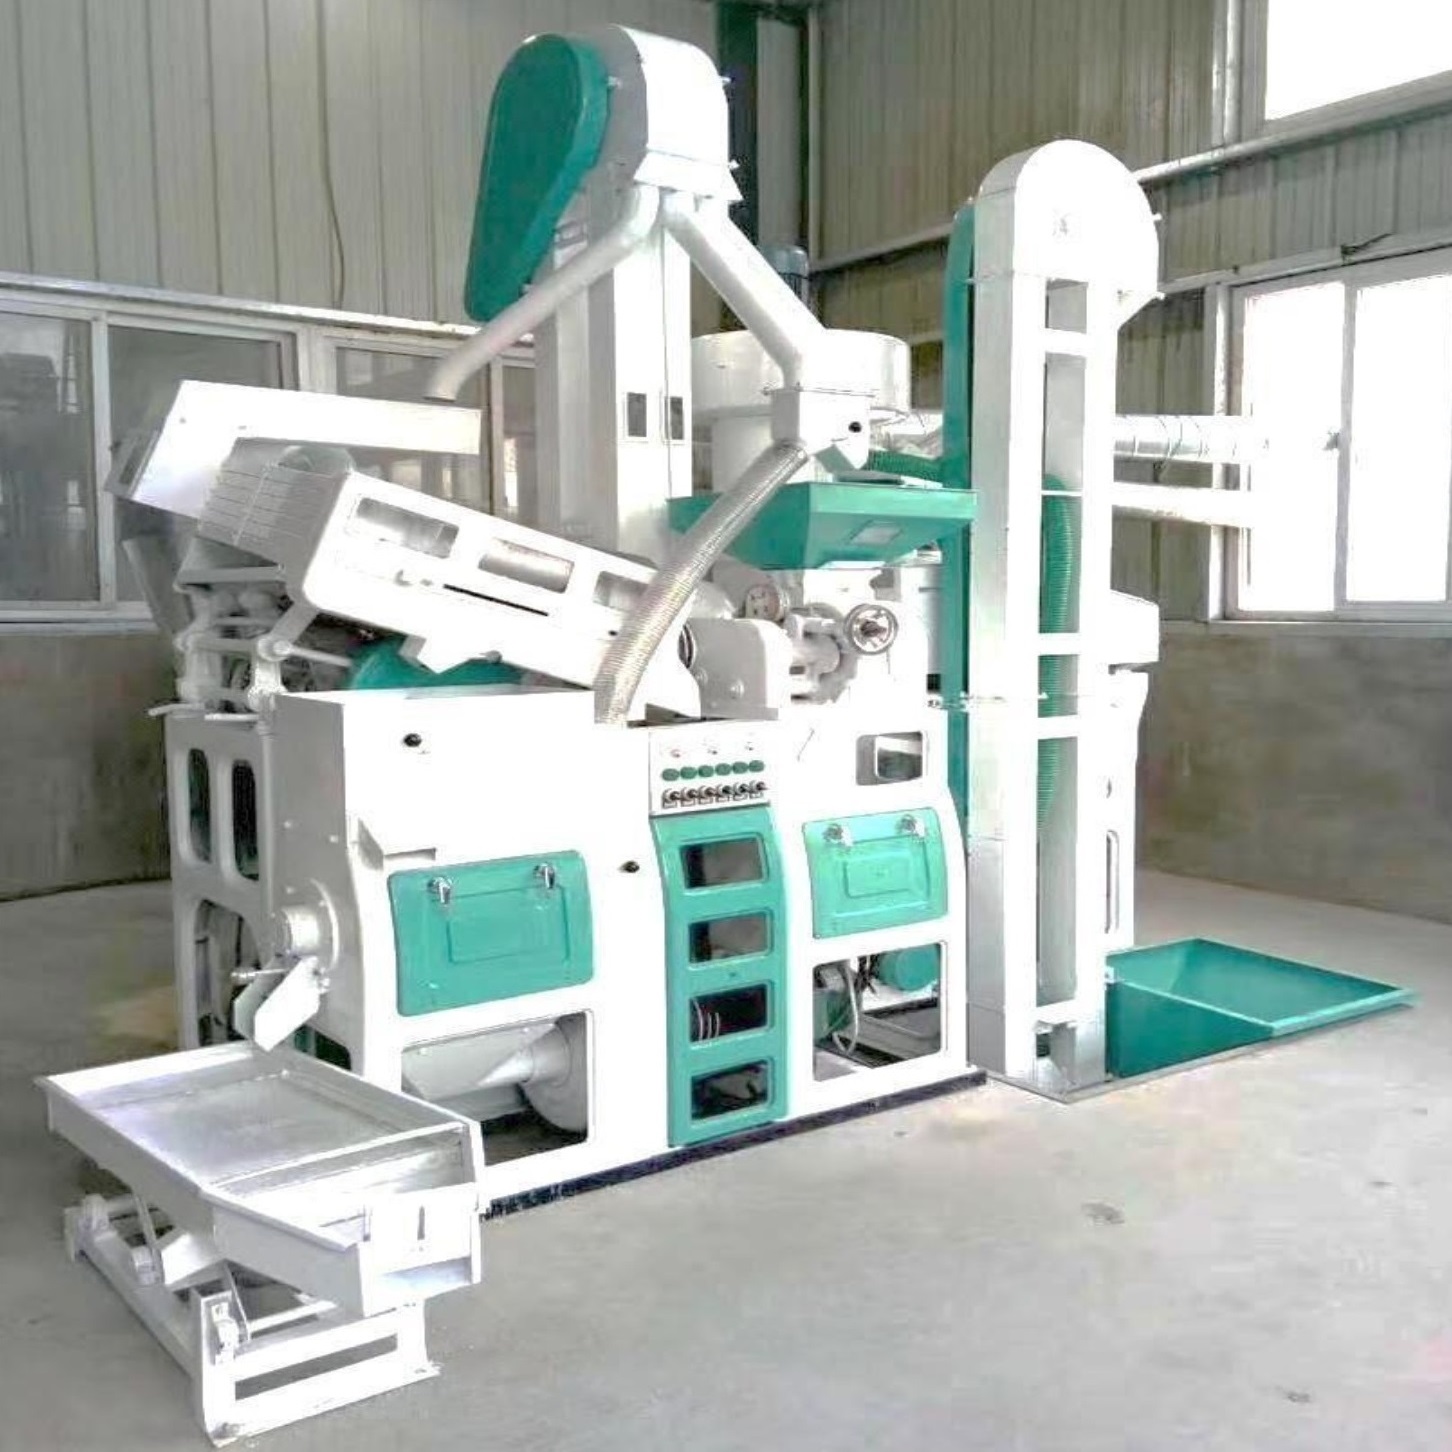
The Combined Rice Mill serves as the optimal middle-ground solution. It consolidates cleaning, de-stoning, hulling, whitening, and crushing into a single, space-efficient footprint. This setup drastically reduces capital expenditure compared to large-scale modular plants. It simplifies the mechanical workflow so operators do not need advanced engineering degrees to run the equipment. You get continuous processing from raw paddy to graded white rice, transforming raw agricultural yield into market-ready products efficiently.
Integrated Efficiency: A combined rice mill reduces facility footprint by up to 60% while executing 4-in-1 processing (cleaning, hulling, milling, and grading) continuously.
Scalable Capacities: Systems range from a mini combined rice mill (e.g., 500-1000kg/h) for small rural co-ops to 25T/D units for medium-scale regional processing.
Byproduct Monetization: Modern integrated machines automatically separate premium head rice, broken rice, and bran, utilizing built-in crushers to process husks into profitable animal feed.
Implementation Reality: Success relies heavily on proper site preparation (foundation pits, structural racks), securing local permits, and precise calibration of huller clearance and whitener pressure during the first run.
The Strategic Role of Combined Milling in Cooperative Processing
Defining success for a cooperative milling operation requires looking at daily metrics. Consistent daily throughput matters most during peak harvest. You cannot afford machine downtime when paddy arrives by the truckload. Minimal grain breakage directly impacts cooperative revenue. Low energy consumption per ton keeps operational overhead manageable. Non-engineer staff will operate and maintain this equipment daily, so the machinery must be intuitive and robust.
Cooperatives pool resources to maximize returns for their members. When members sell raw paddy to large commercial mills, they lose the value-added margin of processed white rice. By bringing the milling process in-house, the cooperative captures this margin. However, building a massive commercial facility requires millions in capital. This is where the combined unit shines. It delivers the necessary processing quality without the massive debt burden.
Traditional multi-stage standalone setups often fail to meet these specific cooperative needs. They require complex bucket elevators to move grain between separate machines. They consume massive floor space. A standard standalone plant requires a building at least 10 meters high to accommodate the long bucket elevators. It needs separate rooms for cleaning, hulling, and polishing to manage dust. You have to hire specialized operators to monitor each individual processing stage.
An integrated rice milling machine solves these exact problems. It links every processing stage internally. Gravity and short internal elevators move the grain. This eliminates long conveyor runs and centralizes the control panel for a single operator. An integrated unit condenses this entire workflow into a frame that often stands less than 3 meters tall. You can install it in an existing agricultural shed. You do not need to construct a custom steel building. This slashes the initial civil engineering costs by a massive margin.
You must weigh conceptual trade-offs when selecting equipment. A combined unit offers compact convenience and significantly lowers daily staffing requirements. Modular standalone industrial plants offer hyper-customization, allowing you to swap out individual machines easily. A combined unit sacrifices some of that modularity for space savings. For most agricultural cooperatives, the compact footprint wins. The lower initial setup complexity provides a faster path to production.
Operational Feature
Standalone Modular Plant
Integrated Combined Mill
Facility Footprint
Requires massive floor space and high ceilings (10m+).
Highly compact; fits in standard agricultural sheds (3m).
Installation Time
Takes weeks; requires extensive alignment and civil works.
Takes days; arrives mostly pre-assembled on a skid.
Operator Skill Level
Requires specialized technical training for each stage.
Basic mechanical aptitude is sufficient for a single operator.
Internal Conveyance
Complex external bucket elevators and augers.
Short, internal gravity-fed or enclosed lifts.
Maintenance Focus
Multiple independent drive systems and gearboxes.
Centralized motor and shared drive belts.
Technical Evaluation: Core Components and Capabilities
Multi-Functional Processing Stages
Understanding the flow of grain through the system ensures proper operation. The process begins with pre-cleaning and de-stoning. Raw paddy contains straw, dust, and stones from the field. Vibrating screens remove the large impurities. A gravity destoner uses airflow and vibration to separate heavy stones. The gravity destoner relies on fluidization. A fan blows air up through a vibrating screen. The lighter paddy floats on this cushion of air and flows down the incline. The heavier stones sink to the screen surface and travel up the incline due to the vibration. Adjusting the airflow and screen angle dictates success here. If the air is too strong, paddy blows out with the stones. If it is too weak, stones flow down with the paddy and destroy the huller.
The grain then moves to the rubber roller hulling stage. Hulling efficiency dictates the overall throughput of the machine. Two rubber rollers spin at different speeds. They create a shearing force that strips the husk from the paddy. You must evaluate the adjustable roller tension carefully. Different paddy varieties require different pressure settings. Long-grain varieties need wider clearances than short-grain varieties. Incorrect tension either leaves paddy unhulled or crushes the grain completely.
Whitening and polishing transform brown rice into white rice. The milling chamber uses an emery or iron roll. It rubs the bran layers off the grain. The emery roll acts like a grinding wheel. The grit size of the emery roll determines the finish of the rice. Coarse grit removes bran quickly but leaves deep scratches on the kernel. Fine grit polishes the kernel but generates more heat. You must select the correct emery roll based on your target market. Premium markets demand a smooth, glossy finish. The chamber forces grains to rub against each other and the outer screen. This process generates heat. High-quality machines minimize thermal stress on the grain. Excessive heat causes the rice kernels to crack and break. Proper airflow through the whitening chamber pulls away the bran and cools the rice simultaneously. This preserves your head rice yield.
Byproduct Management and Integrated Crushing
Modern machines handle byproduct separation automatically. The mechanics of simultaneous separation rely on internal aspirators and sieves. The machine isolates clean white rice, fine bran, and broken rice into separate chutes. You do not need secondary sorting machines for basic grading. The aspirator pulls light bran away from the heavier rice kernels. The grading sieve lets broken grains fall through while whole grains pass over the top.
Integrated crushing mechanisms add significant value to the operation. The machine pulverizes raw husks into fine bran in one continuous pass. It eliminates the need for a separate hammer mill. The built-in crusher uses high-speed blades to break down the tough outer husks. This mixes the crushed husk with the nutrient-rich bran from the whitening stage. You produce a ready-to-sell animal feed byproduct instantly. This maximizes the total yield from every ton of raw paddy.
Capacity Sizing for Cooperatives
Selecting the right machine size depends entirely on cooperative member yield. You must calculate the peak daily harvest volume. A small combined rice mill typically processes 500 to 1500 kilograms per hour. This size fits local village cooperatives perfectly. It handles daily deliveries from smallholder farmers without creating a massive backlog. You can run it for a few hours a day based on demand.
Larger regional cooperatives require more robust solutions. A 25-ton per day continuous operation system suits centralized hubs. These machines run for 16 to 24 hours straight during peak season. They require dedicated loading infrastructure. Machine capacity must align with your wet paddy intake and drying speed. If your cooperative harvests 10 tons of wet paddy a day, you must dry it down to 14% moisture before milling. If your batch dryer only handles 5 tons a day, buying a 20-ton per day mill wastes capital. The mill will sit idle waiting for dry paddy. You must map the entire workflow from the weighbridge to the bagging scale.
Consider the bagging operation as well. A mill producing 1 ton of white rice per hour fills twenty 50kg bags. One operator can easily manage this manual bagging rate. If you scale up to a 2-ton per hour system, manual bagging becomes a bottleneck. You will need to invest in automated weighing and bagging scales. Always factor downstream logistics into your capacity sizing decisions.
Follow these steps to determine your capacity needs:
Audit the total acreage harvested by all cooperative members.
Calculate the average yield per acre in your specific region.
Determine the peak harvest window, usually spanning three to four weeks.
Divide the total expected tonnage by the working days in the harvest window.
Factor in a 20% buffer for unexpected delivery surges or weather delays.
Site Preparation, Infrastructure, and Compliance
Space, Layout, and Foundation
Physical prerequisites dictate the success of your installation. You must pour a perfectly level concrete foundation. Industrial milling equipment generates significant vibration. Uneven floors cause structural fatigue and premature bearing failure. Do not use standard residential concrete for the foundation. Specify a high-strength industrial mix, minimum 3000 PSI. Reinforce the slab with a steel rebar grid, not just wire mesh. The constant harmonic vibration of the milling head will crack weak concrete within months. Once the concrete cracks, the machine loses its level, and bearings start failing. Allow the concrete to cure for a full 28 days before anchoring the machine. Rushing the installation on green concrete leads to anchor pull-out.
The layout must allow clear access to all sides of the machine. Operators need room to change screens, replace belts, and clear jams. Never push the machine flush against a wall. Leave at least one meter of clearance around the entire perimeter.
Specific pit digging requirements apply to larger units. A standard 25-ton model often requires foundation pits. A common dimension is 85x85x60cm. These pits house the boot of the bucket elevator. If the pit is too shallow, the elevator cannot scoop the grain properly. If it is too deep, routine maintenance becomes impossible. You must also install structural rack stabilization. Bolt the main frame securely to the concrete floor using heavy-duty anchor bolts. Use non-shrink epoxy grout to lock the bolts into the concrete slab permanently.
Power Supply and Electrical Load Management
Electrical infrastructure requires careful planning before the machine arrives. Commercial units demand stable 3-phase power. The motors draw heavy starting currents. Your main breaker panel must handle these initial spikes without tripping. A mini combined rice mill might operate on single-phase power. This makes it ideal for remote locations with limited grid infrastructure. Always verify the motor nameplate ratings against your local supply.
Use heavy-gauge copper wire for all motor connections. Undersized wires create resistance, drop the voltage, and generate heat. Route all cables through rigid metal conduit. Rodents in agricultural facilities will chew through exposed PVC wiring, causing short circuits and fires. Install a dedicated grounding bus bar in the main electrical panel. Connect the machine frame, the motor casings, and the control panel enclosure to this bus bar.
Rural areas frequently suffer from grid fluctuations. Voltage drops destroy electric motors quickly. You must install industrial voltage stabilizers. A phase-failure relay is also mandatory for 3-phase systems. If one power phase drops out, the relay shuts down the motor instantly. This prevents the motor from overheating and burning out the windings. Proper grounding of the entire machine frame prevents static electricity buildup during the milling process. Drive copper grounding rods at least two meters into the earth outside the facility.
Permits, Zoning, and Environmental Compliance
Setting up a processing plant requires navigating local regulations. You must secure agricultural processing permits before pouring concrete. Zoning laws often dictate where you can operate machinery. Milling equipment generates considerable noise. You cannot place these facilities directly adjacent to residential housing without soundproofing. Check your local municipal codes regarding industrial noise limits.
Environmental compliance focuses heavily on dust management. Milling rice creates fine, combustible dust. You must install mandatory dust extraction systems. Cyclone separators capture the airborne particulate matter. This ensures operator safety and prevents respiratory issues. It also keeps the facility clean. Accumulated dust poses a severe fire hazard. Local fire marshals will inspect your cyclone and baghouse setups before granting operational approval. Ensure all exhaust stacks clear the roofline by at least two meters to disperse clean air properly.
Installation, Calibration, and First-Run Testing
Assembly Sequencing
Installation follows a strict mechanical sequence. You must firmly install all structural components and base racks first. Level the main frame using steel shims and a machinist's level. Do this before mounting any heavy motors or milling heads. Bolting heavy components to an unlevel frame warps the chassis. Once the frame is secure, install the elevator legs and the destoner assembly.
When installing the bucket elevator belts, ensure the buckets face the correct direction of travel. The belt must track perfectly in the center of the top and bottom pulleys. If the belt rubs against the side of the elevator casing, it will fray and snap. Adjust the tracking using the tension bolts on the bottom pulley. Run the elevator empty for an hour to verify the tracking before introducing any grain.
Mount the main drive motors last. Align the pulleys perfectly using a laser alignment tool or a straight edge. Misaligned pulleys destroy drive belts in a matter of hours. Tension the belts according to the manufacturer's specifications. Do not over-tighten them. Excessive tension ruins motor bearings. Finally, connect the ductwork for the cyclone separators. Ensure all pipe joints are sealed with silicone to prevent dust leaks.
Staffing and Operator Training
Cooperative members require structured training before operating the equipment. Teach safe machine operation first. No loose clothing or jewelry is allowed near the drive belts. Enforce daily maintenance checks strictly. Operators must inspect belt tension, lubricate bearings, and clean the destoner screen every morning. They must empty the dust collection bags before they overflow.
Emergency procedures require practice. Every operator must know the location of the main emergency shut-off switch. If a stone bypasses the cleaner and jams the huller, the operator must cut the power instantly. Train staff to listen to the machine. A healthy mill hums steadily. Grinding noises, sudden vibrations, or squealing belts indicate immediate mechanical trouble. Early detection prevents catastrophic equipment failure.
Calibration (Implementation Risks)
The first run carries significant implementation risks. Most setup failures happen during initial calibration. You must adjust the feed gate correctly. Never open the feed gate fully on an empty machine. Start with a trickle of paddy. Let the machine fill gradually. If you flood the huller, the motor will stall. Adjust the huller clearance precisely. Bring the rubber rollers together until you hear them barely touch, then back them off slightly.
Dialing in the milling room pressure takes patience. The resistance weight on the discharge gate controls this pressure. Too much pressure crushes the rice, resulting in high breakage rates. Too little pressure leaves bran on the kernel, resulting in brown, unpolished rice. You must find the sweet spot for your specific paddy variety. Adjust the weight in small increments. Inspect the output after every adjustment.
Troubleshooting the First Production Run
Identify early warning signs of improper setup immediately. Excessive bran in the white rice indicates poor aspiration. Check the airflow gates on the suction fan. If the fan cannot pull enough air, the bran stays mixed with the rice. High vibration usually means the machine is not bolted down tightly. It can also indicate an unbalanced milling roller. Stop the machine and check all anchor bolts.
Motor overheating requires instant mitigation. If the main drive motor feels too hot to touch, you are overloading the machine. Close the feed gate slightly to reduce the grain flow. Check the voltage at the panel. Low voltage causes motors to draw higher amps and overheat. Verify that the drive belts are not slipping. Slipping belts transfer heat directly to the motor shaft. Fix these issues before resuming production.
If dust blows out of the top exhaust of the cyclone, the bottom airlock is leaking. The cyclone relies on a strict vortex to separate the dust from the air. Any air leaking into the bottom of the cone destroys this vortex. Check the rubber seals on the rotary airlock valve. Replace them if they are worn or torn. Ensure the dust collection bags are made of breathable fabric. If the fabric is too tight, backpressure builds up and chokes the cyclone.
Symptom
Probable Cause
Immediate Action
High percentage of broken rice
Excessive milling room pressure or tight rollers.
Reduce discharge weight; widen rubber roller gap.
Unhulled paddy in output
Rubber rollers worn out or gap too wide.
Tighten roller clearance; replace rollers if smooth.
Bran mixed with white rice
Clogged aspirator screen or weak fan suction.
Clean internal screens; open fan air intake valve.
Elevator belt slipping
Bucket elevator jammed with grain at the boot.
Stop machine; open bottom hatch and clear grain.
Excessive machine vibration
Loose anchor bolts or unbalanced emery roll.
Tighten foundation bolts; inspect roll for damage.
Conclusion
To successfully deploy a milling system for your cooperative, execute the following steps:
Conduct a site audit to measure available floor space, ceiling height, and foundation integrity.
Calculate your cooperative's peak harvest daily tonnage to determine the exact machine capacity required.
Consult with a local electrician to verify your facility's phase power and breaker capacity.
Request detailed technical specification sheets and installation manuals from qualified manufacturers.
FAQ
Q: What is the average capacity of a small combined rice mill?
A: A small unit typically processes between 500 kilograms and 1.5 tons per hour. This capacity perfectly suits localized cooperative use. It handles the daily harvest of smallholder farmers without requiring massive storage silos. You can run it intermittently based on daily paddy deliveries.
Q: How does an integrated rice milling machine separate bran and broken rice?
A: The machine uses internal grading screens, aspirators, and cyclone systems. These operate simultaneously during the milling phase. The aspirator fan pulls light bran away from the heavy kernels. The grading sieve allows small broken grains to fall through while whole head rice passes over the top into the bagging chute.
Q: What are the power requirements for a mini combined rice mill?
A: Ultra-compact mini units often run on standard single-phase power (220V). This makes them accessible for rural areas. However, as you scale up to standard cooperative models (like 1-ton per hour units), you must transition to 3-phase industrial power (380V/415V) to handle the heavier motor loads.
Q: Do I need a special foundation to install a combined rice mill?
A: Yes. You need a reinforced, perfectly level concrete base to dampen heavy vibrations. Larger models require specific pit dimensions, such as 85x85x60cm. These pits house under-machine conveyors, bucket elevator boots, or structural stabilization racks. Never install the machine on dirt or weak wooden floors.
Q: How often do the rubber rollers need to be replaced?
A: Rubber rollers are high-wear items. You typically replace them after processing 100 to 150 tons of paddy. The exact lifespan depends heavily on the hardness of the paddy variety and the cleanliness of the grain. High stone content will destroy the rollers prematurely.
Q: Can a combined rice mill process parboiled rice?
A: Yes, but it requires specific adjustments. Parboiled rice is significantly harder than raw paddy. You must install hardened milling screens and specialized emery rollers. Standard iron rollers may struggle with the hardened bran layer of parboiled grain, leading to higher wear and lower throughput.
Q: Do I need specialized staff to operate a combined rice mill?
A: No. While basic mechanical aptitude helps, these machines are designed for ease of use. Cooperative members can operate them effectively after receiving standard operational and safety training. They only need to learn how to adjust feed gates, monitor belt tension, and clear simple blockages.