High-volume agricultural packaging lines hit a hard wall when material feeding systems cannot keep up with the weighing mechanisms. Single-hopper configurations force an intermittent flow. This sequential wait-to-fill process creates micro-delays during every cycle. Over a standard shift, these brief pauses compound into massive lost tonnage and severe operational inefficiency. The limitation rarely lies in the load cells or the bagging clamps. Instead, the bottleneck is the physical movement of the grain.
To eliminate feed latency, facility managers must look at structural upgrades. The dual feeding hopper architecture removes the dead time inherent in older designs. It balances high-speed throughput with precise dosing accuracy. By utilizing parallel material staging, facilities maintain constant head pressure and achieve continuous discharge. Upgrading the feeding mechanism transforms the packaging line into an uninterrupted operation, maximizing output without sacrificing the strict weight tolerances required on the floor.
- Continuous Flow Dynamics: Dual feeding systems allow for simultaneous staging and discharging, eliminating the dead time inherent in sequential single-hopper filling.
- Precision Dosing: Utilizing parallel hoppers enables dedicated coarse (bulk) and fine (dribble) feeding, drastically reducing product giveaway without sacrificing speed.
- Automated Replenishment: Integrated level sensors automatically trigger upstream supply when a hopper runs low, ensuring uninterrupted production cycles.
- Spillage Reduction: Larger, optimized target areas and synchronized outlet valves minimize material loss and dust generation during the transfer process from upstream screeners and conveyors.
- ROI Thresholds: Upgrading to dual hopper configurations becomes cost-justifiable when facility throughput requirements exceed the mechanical limits of standard single-lane systems.
Operational Mechanics: How Dual Feeding Hoppers Function in High-Volume Environments
Continuous vs. Intermittent Material Flow
Sequential feeding relies on a wait-to-fill mechanism. The system must pause discharging to refill the hopper. This intermittent flow disrupts the packaging rhythm and forces the bagging operator or automated bagger to wait. Parallel feeding changes this dynamic entirely. Dual hoppers allow the system to fill while discharging simultaneously. One chamber stages the incoming material from the bucket elevator. The other chamber actively feeds the weighing buckets below.
This parallel action maintains a constant head load. Consistent pressure is vital for granular materials like rice. It ensures steady flow rates into the weighing buckets. When head pressure fluctuates in a single hopper, material density shifts at the discharge gate. Dual hoppers stabilize this pressure by keeping the active feeding chamber adequately full. The weighing controller receives a uniform stream of product. This mechanical consistency directly improves both cycle speed and fill accuracy.
| Flow Characteristic |
Single Hopper (Intermittent) |
Dual Hopper (Continuous) |
| Head Pressure |
Highly variable as material depletes |
Stable and consistent |
| Cycle Dead Time |
High (waiting for refill) |
Zero (simultaneous staging) |
| Material Density at Gate |
Fluctuates with volume |
Uniform |
| Upstream Integration |
Requires start/stop signaling |
Allows continuous upstream operation |
Automated Level Control and Upstream Replenishment
Modern feeding systems rely on a strict sensor-based feedback loop. Capacitive or rotary paddle level sensors monitor the material volume continuously inside the staging hopper. When the material drops below a specific threshold, the sensor detects the change immediately. It sends a signal to the programmable logic controller (PLC). The PLC then automatically triggers the upstream elevators or conveyors to supply more material.
Operators do not need to intervene manually to keep the machine fed. The continuous replenishment prevents the starvation of the weighing heads. Starvation causes severe delays, inaccurate fills, and triggers fault alarms. By maintaining system equilibrium, the automated loop ensures the packaging line never waits for product. The upstream supply matches the downstream discharge rate perfectly, creating a seamless transfer of grain from the silo to the bag.
Coarse and Fine Dosing Synchronization
Achieving exact target weights at high speeds requires a two-stage feeding process. Dual hoppers excel at this synchronization. One hopper handles the rapid bulk filling. We call this the coarse feed. It rapidly dumps material to reach approximately 90% of the target weight. The pneumatic gates open fully, allowing maximum flow. Speed is the primary goal during this phase to keep the bags per minute (BPM) high.
The second hopper manages the precision dribble feeding. We call this the fine feed. It carefully meters out the final 10% of the material. Automated outlet valves control this process. They open and close based on real-time load cell feedback. The pneumatic gates adjust their aperture instantly, restricting the flow to a narrow stream. This synchronized mechanical action ensures the bag fills quickly but finishes with pinpoint accuracy, hitting the target weight without going over.
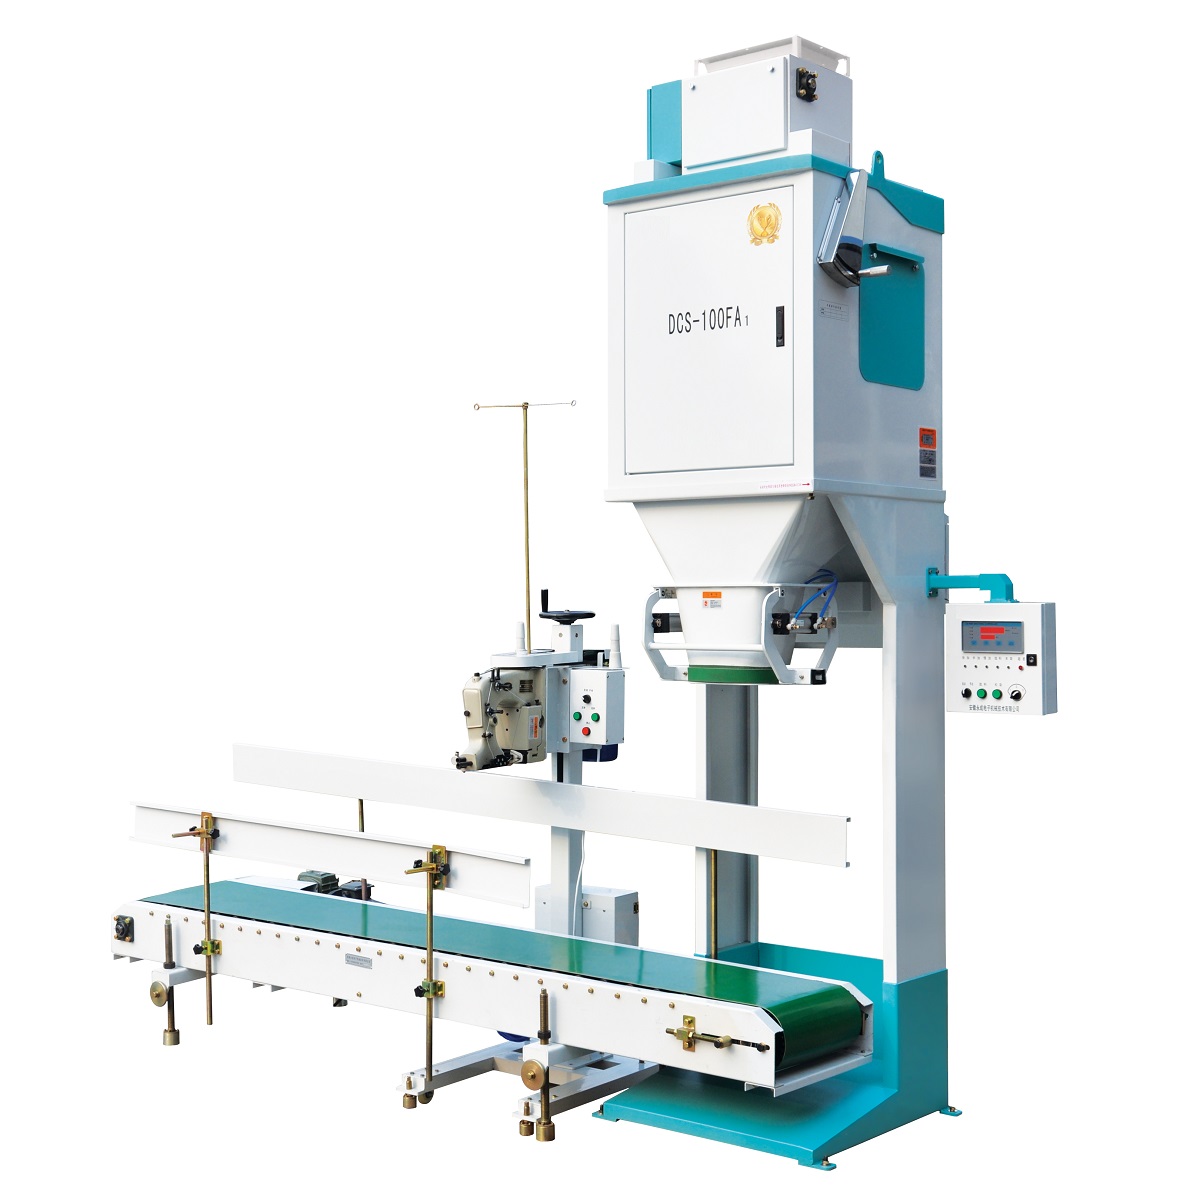
Throughput Optimization and Multi-Lane Stability (Bags per Minute)
Removing feed latency changes the packaging equation entirely. Cycle speeds increase dramatically when the machine stops waiting for material. An Electronic Rice Packing Scale equipped with dual hoppers can push throughput to its mechanical limits. Facilities often see bag-per-minute rates jump significantly compared to single-hopper setups. When you eliminate a two-second delay on every bag, you gain hours of active production time over a single week.
Multi-lane or dual-feed setups maximize this advantage. They allow multiple weighing heads to work simultaneously. This stabilizes production rates across the entire shift. Single-lane bottlenecks often suffer from product overlap issues where material bridges over the gate. Dual hoppers separate the material streams. This prevents bridging and ensures each weighing lane operates independently. If one lane requires maintenance, the other can often continue running, preventing a total line shutdown.
- Cycle Time Reduction: Eliminates the 1-3 second wait time for hopper refilling between bag drops.
- Independent Lane Operation: Allows one side of a dual system to run while the other is paused for roll changes or maintenance.
- Consistent BPM: Stabilizes the bags-per-minute output, allowing plant managers to forecast daily tonnage accurately.
- Upstream Synchronization: Keeps bucket elevators running at a steady amperage, reducing wear on upstream motors.
Minimizing Product Giveaway (Accuracy Metrics)
Overfilling bags destroys profit margins. Even a few extra grams per bag add up quickly when you run thousands of bags a shift. Over a fiscal year, this product giveaway represents massive financial loss. Accuracy is not just a quality metric; it is a strict retention of revenue. Dual-feed mechanisms tighten the standard deviation of every fill by controlling the final dribble phase with absolute authority.
High-speed single-hopper systems struggle with "in-flight" material. This is the product currently falling through the air when the gate closes. Calculating this in-flight volume is difficult when head pressure varies. Dual hoppers stabilize the head pressure. The fine dosing gate can close with absolute precision because the flow rate is predictable. This prevents calculation errors, keeps fills exactly on target, and stops the facility from giving away free grain.
Reducing Spillage and Material Waste
Spillage creates environmental hazards, attracts pests, and wastes valuable product. Single hoppers often present a small target for upstream conveyors. Material bounces or spills over the edges during high-speed transfers. Dual hoppers provide a much larger, more controlled target area. Upstream screeners and elevators can discharge material safely without missing the intake zone.
Integration of physical containment further reduces waste. Facilities install skirtboards around the transition zones. Transition modifications help contain the granular flow. This prevents dust generation and environmental contamination on the packaging floor. Keeping the facility clean reduces maintenance downtime, prevents slip hazards, and preserves the quality of the packaged product. Dust extraction ports can also be integrated more easily into the larger shroud of a dual hopper system.
System Comparisons: Single vs. Dual Hopper Configurations
Many facilities start their automation journey with a semi automatic packing scale. These systems rely on single feed points and manual bag placement. They have a strict operational ceiling. An operator can only position bags so fast. The single hopper must wait for the operator to clamp the bag, and the operator must wait for the hopper to refill after the drop. This mutual waiting game caps the maximum daily output.
However, these systems still hold value in specific scenarios. Low-volume runs do not require continuous flow. Specialty batching, such as organic or flavored rice, often demands manual oversight and frequent cleanouts. In these cases, a single hopper remains sufficient. Upgrading to dual hoppers makes sense only when the manual bagging process is no longer the primary bottleneck and the facility needs to push higher volumes.
Upgrading requires clear criteria. Facility managers must evaluate labor availability, throughput demands, and strict tolerance requirements. When manual labor cannot keep pace with production goals, automation becomes necessary. High throughput demands continuous material flow. Strict tolerances demand precision dosing that manual gates cannot provide.
An intelligent packing scale takes dual feeding to the next level. It utilizes predictive algorithms to monitor the process. The controller adjusts the vibratory feed rates automatically. It bases these adjustments on real-time material density variations. If a new batch of rice is slightly heavier or has higher moisture content, the system adapts instantly. It modifies the coarse and fine feed timing without operator input, ensuring the first bag of the new batch is just as accurate as the last.
| System Type |
Feed Mechanism |
Operator Dependency |
Throughput Capacity |
Best Use Case |
| Semi-Automatic (Single Hopper) |
Gravity or single vibratory pan |
High (manual bag clamping) |
Low to Medium (4-8 BPM) |
Specialty runs, low-volume facilities |
| Intelligent (Dual Hopper) |
Parallel coarse/fine dosing |
Low (automated adjustments) |
High (12-20+ BPM) |
High-volume industrial milling operations |
Hopper Design, Transition Angles, and Vibratory Efficiency
The geometry of the hopper dictates material flow. Granular products like rice require specific angles to prevent stagnation. Steep cone angles (typically 60 degrees or more) promote mass flow. In mass flow, all material moves simultaneously, preventing older grain from sitting at the edges. Shallow transitions often cause funnel flow, leading to bridging or rat-holing. Product overlap occurs when grains lock together in dead zones, requiring operators to hit the hopper with a mallet to restore flow.
Modifying the hopper transition directly impacts vibratory feeding efficiency. Flow aids and vibratory drives must transfer energy effectively into the grain. If the hopper design is flawed, the vibration dissipates into the steel frame instead of the product. Proper transition angles ensure the vibrational energy moves the rice smoothly toward the gate. This eliminates dead zones and keeps the rice packing machine running at peak capacity without manual intervention.
Material Construction: Stainless Steel vs. Specialized Plastics
Hopper fabrication materials influence both performance and compliance. Food-grade stainless steel, specifically 304 or 316 grades, is the industry standard. It offers immense durability, resists corrosion, and allows for aggressive sanitation washdowns. However, some facilities explore specialized anti-static plastics or Ultra-High Molecular Weight (UHMW) polyethylene liners for specific applications.
The choice of material impacts the friction coefficient. Lower friction allows rice to slide easily without breaking. Grain breakage degrades the final product quality, turning premium whole grain into lower-value broken rice. Stainless steel provides a smooth surface, but anti-static plastics prevent dust accumulation on the walls. Facilities must balance sanitation compliance with the physical characteristics of the grains they process to minimize degradation.
Load Cell Integration and Processing Latency
Dual feeding mechanisms move fast. The load cells must keep pace. Standard load cells may suffer from processing latency, causing the gate to close a fraction of a second too late. High-frequency sampling rates are mandatory. The load cell must read the weight hundreds of times per second. This ensures the controller knows exactly when the target weight is approaching.
Communication speed between the weighing controller and the pneumatic hopper gates is equally critical. If the load cell detects the target weight, but the signal delays by just 50 milliseconds, the bag overfills. Low-latency processing ensures the fine dosing gate shuts instantly. Upgrading to strain gauge load cells with advanced digital filtering secures the accuracy metrics required by modern high-speed facilities.
Material Compatibility and Degradation
Not all rice flows the same way. Long-grain rice behaves differently than short-grain varieties. Jasmine rice can carry slightly different surface friction due to its starch content. Broken rice tends to pack tightly and resist flow, increasing the risk of bridging. Dual feeding systems must handle these different grades without causing mechanical damage or requiring constant recalibration.
Excessive friction during the bulk and dribble phases causes degradation. The grains rub against each other and the hopper walls. Proper hopper geometry and optimized vibratory frequencies mitigate this risk. The system must move the material gently but swiftly. Evaluating material compatibility during the equipment selection phase ensures the final packaged product retains its premium appearance and grade.
Implementation Realities and Adoption Risks
Footprint and Facility Integration Constraints
Dual hopper systems require more physical space. They demand increased vertical and horizontal clearance compared to standard single-hopper units. The parallel structure widens the machine footprint on the floor. More importantly, the need for upstream staging increases the vertical drop requirement. Facilities cannot simply swap a single hopper for a dual setup without measuring the available space first.
Conducting a strict facility audit is necessary before procurement. Measure existing ceiling heights accurately. Evaluate the discharge height of current upstream bucket elevators. Ensure the new dual hopper system fits within the existing structural framework or mezzanine. Ignoring footprint constraints leads to costly installation delays, forced facility modifications, or the need to purchase custom low-profile elevators.
Maintenance Overhead and Cleaning Protocols
Adding a second hopper increases mechanical complexity. Facilities must maintain two independent feed mechanisms. This means double the pneumatic cylinders, double the gate valves, and double the vibratory drives. The preventive maintenance schedule must expand to cover these additional moving parts. Air quality becomes critical; moisture in the air lines will destroy pneumatic cylinders rapidly.
Sanitation requirements also increase. Cross-contamination between different rice varieties (e.g., mixing white rice with parboiled) is unacceptable. Cleaning dual hoppers takes more time. Emphasize the accessibility of dual hopper clean-out doors during the procurement phase. Operators must be able to open, inspect, and clean both chambers quickly during product changeovers without requiring specialized tools.
Operator Training and Calibration Requirements
Advanced machinery requires skilled operators. There is a distinct learning curve associated with dual feed systems. Operators must learn how to navigate the Human-Machine Interface (HMI) to calibrate coarse and fine feed timing accurately. They must set automated replenishment thresholds and understand how to adjust the pre-act (in-flight) compensation values.
Diagnostic skills become paramount. If the hoppers discharge asynchronously, the operator must know how to troubleshoot the issue. They need to understand pneumatic pressure settings, filter regulators, and load cell calibration procedures. Investing in comprehensive operator training ensures the facility actually achieves the efficiency gains the machinery promises, rather than fighting constant fault codes.
Conclusion
Dual feeding hoppers represent a critical architectural requirement for high-volume facilities. When the financial loss of product giveaway and feed latency outweighs the capital expenditure of advanced machinery, upgrading becomes essential. Parallel feeding stabilizes head pressure, maximizes throughput, and secures dosing accuracy. Decision-makers should evaluate their current limitations logically. Assess target bags per minute, acceptable margins of error, available floor space, and upstream screener compatibility. If single-lane bottlenecks restrict daily tonnage, a dual hopper system aligns perfectly with aggressive operational goals.
- Conduct a detailed time-study on current packaging lines to identify exact micro-delay durations between bag fills.
- Calculate the annual financial loss attributed to product giveaway from single-hopper in-flight calculation errors.
- Audit facility ceiling heights and upstream elevator discharge points to confirm vertical clearance for a dual-hopper footprint.
- Develop an updated preventive maintenance schedule that accounts for the additional pneumatic cylinders and vibratory drives.
FAQ
Q: What is the primary advantage of a dual feeding hopper on an electronic rice packing scale?
A: The primary advantage is the simultaneous execution of bulk and dribble feeding. This parallel action eliminates wait times, maximizing both speed and accuracy. It also maintains constant head pressure, ensuring a steady, predictable flow of material into the weighing buckets without the density fluctuations common in single hoppers.
Q: Can a semi automatic packing scale be retrofitted with dual hoppers?
A: Retrofitting is generally impractical. Semi-automatic controllers often lack the processing speed and I/O ports for dual inputs. Structural framework constraints usually prevent mounting a second hopper safely. Furthermore, older systems lack the automated upstream replenishment logic required to keep dual hoppers supplied continuously.
Q: How do dual hoppers prevent material bridging in a rice packing machine?
A: Dual hoppers utilize optimized transition angles and vibratory flow aids to maintain continuous material movement. By separating the flow into coarse and fine streams, the system prevents grain overlap and stagnation. This constant motion stops the rice from locking together and bridging across the discharge gate.
Q: What makes an intelligent packing scale different from standard dual hopper systems?
A: An intelligent packing scale uses self-adjusting algorithms. It automatically calibrates coarse and fine feed times based on real-time flow data. It also integrates seamlessly with automated level sensor feedback, adjusting vibratory frequencies instantly to account for bulk density changes without requiring manual operator intervention.
Q: Do dual feeding systems increase the maintenance requirements of the packaging line?
A: Yes. Dual systems inherently possess more moving parts. Facilities must maintain additional pneumatic cylinders, gate valves, sensors, and vibratory drives. A realistic preventive maintenance schedule is required to inspect air lines, lubricate components, and ensure synchronized discharging remains accurate over time.
Q: How does hopper design impact vibratory feeding efficiency?
A: The shape, transition modifications, and material construction dictate how vibrational energy transfers through the hopper. Proper steep angles ensure the energy moves the product downward efficiently. Incorrect designs absorb the vibration into the frame, creating dead zones that disrupt consistent product flow and cause grain degradation.