Suboptimal impurity separation in commercial milling creates a compounding financial impact that operators cannot ignore. Failing to remove stones, sand, dust, and straw does more than just compromise final product purity. It actively accelerates downstream equipment wear. Heavy impurities destroy emery rollers in whiteners, scratch delicate polishing cylinders, and drastically increase the percentage of broken grains. This operational friction forces plant managers to balance maximum stone removal efficiency against the strict minimization of good grain loss in high-throughput environments. Achieving baseline purity requires precise calibration of aerodynamic and mechanical variables. You must shift the focus from simply operating a destoning unit to actively tuning it for specific paddy conditions and integrating it seamlessly into the broader milling line.
Key Takeaways
Separation accuracy relies on the precise synchronization of three variables: upward airflow, deck inclination, and vibratory stroke frequency.
Excessive air pressure, low air flow channel capacity, or incorrect screen slopes are the primary culprits for high grain loss in the stone discharge chute.
Upgrading to a combined cleaner and destoner can streamline pre-cleaning, but requires independent control mechanisms for air and vibration to maintain accuracy.
System compatibility is crucial; a destoner must integrate smoothly with existing elevators and downstream machinery to prevent feed surging.
Routine auditing of sieve wear, feed distribution, and air channel blockages is mandatory to prevent sudden drops in separation efficiency.
The Mechanics of Density-Based Separation in Rice Cleaning Equipment
Understanding the physics behind density-based separation dictates how well you manage your milling line. Modern rice cleaning equipment relies on specific gravity differentials to stratify materials. Rough rice typically holds a specific gravity of 0.58 to 0.62 g/cm³. Stones, silica, and glass fragments range from 2.4 to 2.8 g/cm³. This massive density gap makes mechanical separation possible, but only if you control the operating environment perfectly. When you master these mechanics, you diagnose separation failures quickly and implement precise corrective actions on the floor.
Defining Separation Accuracy (Success Criteria)
You must establish strict baseline metrics to evaluate machine performance. Separation accuracy is a measurable ratio, not a visual guess. You calculate the percentage of heavy impurities removed against the percentage of sound grain lost in the reject stream. Heavy impurities include stones, glass, and metal fragments. Light impurities encompass dust, straw, and sand. A properly calibrated machine removes 99.5% of heavy impurities while keeping good grain loss in the stone chute below 0.1%. If your reject stream contains excessive white rice, your separation accuracy fails. You must adjust the machine immediately to stop the financial leak. Operators should pull samples from the stone chute every two hours to verify these metrics.
The Interplay of Gravity, Airflow, and Vibration
Density separation relies on the continuous interplay of gravity, upward airflow, and vibratory motion. This process creates a fluidized bed. Upward airflow pushes through the wire mesh sieve at velocities typically between 1.2 and 1.5 meters per second. This air lifts the lighter rice grains, suspending them slightly above the deck. Gravity pulls the heavier stones down, keeping them in direct contact with the textured screen. Simultaneously, the vibratory motion of the deck walks these heavier stones up the inclined slope toward the discharge chute. The lighter, fluidized rice flows downward like a liquid toward the clean grain outlet. If any of these three forces fall out of sync, the fluidized bed collapses, and separation stops entirely.
Feed Consistency and Line Compatibility
Mechanical adjustments mean nothing if your input feed remains erratic. Separation accuracy drops drastically if the incoming paddy surges or starves the deck. Uniform material distribution across the entire width of the sieve is an absolute prerequisite for success. The material bed must maintain a consistent thickness of 15mm to 20mm. If the feed concentrates on one side, air escapes through the empty sections of the screen. This pressure drop causes stones to mix with the clean rice on the overloaded side. Achieving this consistency requires seamless integration with upstream feeding equipment. Surge bins equipped with capacitive level sensors, rotary valves, and properly calibrated elevators ensure a steady, uniform flow into the destoning chamber.
Core Adjustments to Improve Rice Destoner Accuracy
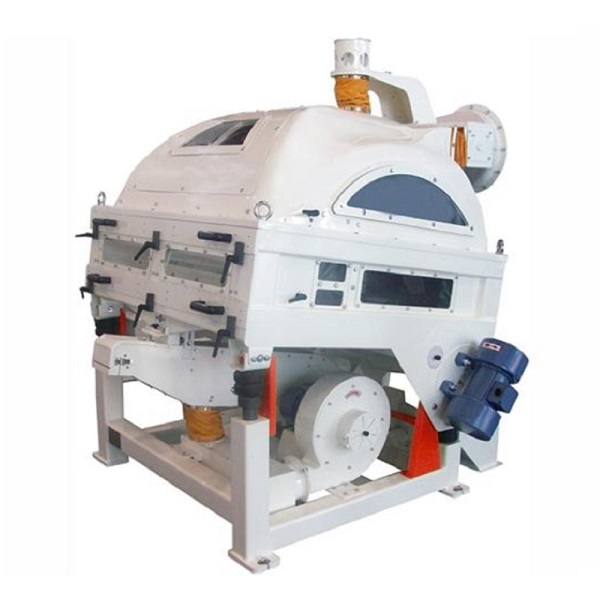
Fine-tuning a Rice Destoner requires a systematic, data-driven approach. You cannot guess at the settings. You must isolate each variable, make incremental changes, and observe the results in the discharge streams.
Calibrating Airflow and Pressure Dynamics
Airflow dictates the fluidization process. You adjust the suction or blower dampers to achieve optimal suspension of the grain. Start by observing the grain bed through the inspection windows. The material should bubble gently, resembling boiling water. If the bed lies flat and sluggish, you lack sufficient air pressure. Open the dampers incrementally.
Structural airflow issues often sabotage performance. Modifying or clearing low air flow channels prevents localized pressure drops. Dust buildup inside the aspiration channels restricts airflow, causing heavy stones to fail to separate. These stones will then discharge with the clean rice. Conversely, you must watch for symptoms of excessive airflow. If the air pressure is too high, it blows sound rice up the incline and into the stone outlet. When you see good grain in the stone chute, immediately reduce the damper opening until the grain recedes. Use a digital manometer to verify that the static pressure inside the hood remains between -150 Pa and -200 Pa.
Follow this exact sequence when calibrating a newly installed unit:
Set the deck angle to the manufacturer's baseline recommendation, typically 7 degrees.
Adjust the inlet feed gate to ensure a uniform 15mm to 20mm material bed depth across the entire screen width.
Increase the fan speed or open the main damper until the paddy bed fluidizes and bubbles evenly.
Fine-tune the eccentric weights or VFD settings to establish the upward migration of heavy stones.
Lock down the dampers and turnbuckles once the stone discharge shows zero sound grain.
Optimizing Deck Slope and Screen Inclination
The longitudinal angle of the destoning deck dictates the speed of material flow and the aggressive nature of the separation. You adjust this angle using the threaded turnbuckles to achieve the optimum degree of separation based on the specific gravity of your paddy. Standard operating angles typically range between 5 and 9 degrees.
You face a constant trade-off when adjusting the slope. Steeper angles increase throughput speed, allowing you to process more tons per hour. However, a steeper slope requires higher vibration intensity and stronger airflow to push the heavy stones upward. This aggressive setting significantly increases the risk of grain loss. Flatter angles provide cleaner separation and protect good grain, but they reduce overall machine capacity. You must find the precise angle that matches your production targets without sacrificing purity. For high-moisture paddy, a flatter angle of 5 to 6 degrees often yields better results by giving the sluggish material more time to stratify.
Tuning Vibratory Motion and Stroke Frequency
Vibration provides the mechanical force necessary to transport stones against gravity. You adjust the eccentric weights or utilize variable frequency drives (VFDs) to alter the vibration amplitude and frequency. Amplitude refers to the length of the stroke, while frequency dictates the speed of the strokes. Most commercial units operate between 400 and 500 strokes per minute with an amplitude of 3mm to 5mm.
Match the vibration intensity to the specific gravity and moisture content of the incoming paddy. Wetter, heavier paddy requires a more aggressive stroke to maintain movement. Drier, lighter paddy needs a gentler frequency to prevent the grain from bouncing uncontrollably. VFDs allow you to make these adjustments on the fly without stopping the machine. If stones pool at the bottom of the deck, increase the frequency by 2 to 3 Hertz. If rice travels up into the stone chute alongside the heavy impurities, decrease the amplitude by adjusting the counterweights.
Sieve Selection and Multi-Layered Configurations
The physical screen forms the foundation of the fluidized bed. Selecting the correct mesh size and wire profile for specific rice varieties is mandatory. Long grain varieties behave differently than short grain varieties. A mesh size optimized for short grain will blind and clog when processing long grain paddy. For long grain rice, operators typically use a 1.2mm by 12mm slotted mesh. For short grain, a 1.5mm round hole mesh provides better fluidization.
Multi-layered sieves dramatically increase separation precision. These configurations stratify the material before it reaches the main destoning deck. The top layers act as scalper screens, removing larger straw, string, and oversized debris. The middle layers sift out fine sand and dust. This pre-cleaning ensures that only rice and similarly sized stones reach the final density-separation phase. Removing these extreme impurities early prevents them from disrupting the delicate airflow required for final stone removal.
Symptom
Probable Cause
Corrective Action
Good rice discharging with stones
Excessive airflow or flat deck slope
Close air dampers slightly; increase deck inclination angle.
Stones discharging with clean rice
Insufficient airflow or blocked channels
Open air dampers; clean aspiration channels and wire mesh.
Uneven material bed (pooling on one side)
Improper feed distribution or unlevel machine
Adjust feed gate for uniform spread; check machine leveling mounts.
Material bed is sluggish and not fluidizing
Blinded screens or low fan speed
Clean the sieves with a brass wire brush; verify fan motor RPM.
Evaluating Advanced Features in Modern Paddy Vibration Cleaners
Procurement teams must look beyond basic specifications when upgrading plant infrastructure. A modern paddy vibration cleaner incorporates advanced engineering features designed to simplify adjustments and maintain strict internal environments. Evaluating these features ensures long-term operational stability and reduces downtime.
Independent Controls for Air and Vibration
Independent controls represent a major upgrade over legacy systems. Older machines often link fan speed and vibration frequency to a single drive mechanism. This creates a tuning nightmare on the floor. If you increase vibration to move heavy stones, you inadvertently increase airflow, which blows good rice into the reject chute. Machines that allow decoupling of fan speed from vibration frequency offer vastly superior tuning capabilities. Operators can adjust the stroke to handle wet paddy while independently dialing back the air pressure to protect lightweight grains. This granular control allows mills to process varying batches of raw material without compromising yield.
Integration of Combined Cleaner and Destoner Systems
Space constraints often force mills to optimize their physical footprint. A combined cleaner and destoner merges pre-cleaning scalper screens with density-separation decks into a single vertical chassis. This integration reduces elevator requirements, lowers overall power consumption, and can save up to 4 square meters of floor space per line.
You must apply strict technical evaluation criteria before installing these units. Ensure the combined unit does not sacrifice the dedicated airflow required for the destoning deck. The pre-cleaning section must have its own aspiration channel, completely separate from the fluidization air used on the destoning deck. If they share a single air chamber, pressure fluctuations from the scalper screen will instantly collapse the fluidized bed below. Furthermore, maintain strict compatibility with existing plant layouts to ensure gravity spouting aligns perfectly without causing feed bottlenecks.
Advanced Discharge Mechanisms
The point of discharge remains highly vulnerable to pressure leaks. Modern units utilize rubber squeeze valves at the heavy impurity discharge points. These valves effectuate clean ejection while maintaining strict internal negative pressure. As stones accumulate, the weight forces the rubber lips open just enough to drop the debris. The vacuum immediately pulls the lips shut again. This prevents ambient air from rushing into the chamber. Air leaks at the discharge point disrupt the fluidized bed, causing localized dead zones where stones fail to separate. Inspecting and replacing these rubber valves is a low-cost maintenance task that yields high returns in separation accuracy. Operators should check the Shore A hardness of these valves monthly, as brittle rubber fails to seal properly.
Implementation Realities: Trade-Offs and Maintenance Risks
Theoretical adjustments fail if you ignore the harsh realities of a commercial milling environment. Equipment degrades, environmental conditions shift, and production demands often push machinery past its limits. You must manage these trade-offs proactively to keep the line running.
Throughput Capacity vs. Separation Precision
Plant managers constantly battle the urge to maximize throughput. You must address the operational reality that pushing a machine beyond its rated capacity destroys separation accuracy. When you overfeed the deck, the material bed becomes too thick. The upward airflow cannot penetrate the dense layer of paddy. The fluidized bed collapses entirely. Without fluidization, stones cannot sink to the screen, and rice cannot float above them. The material simply acts as a solid mass, carrying stones directly into the clean grain outlet. Regardless of how well you adjust the dampers or vibration, an overfed machine will always fail. Respect the volumetric limits of the equipment. A machine rated for 5 tons per hour will fail at 6 tons per hour.
Screen Blinding and Wear Part Replacement
Clogged sieves, known as blinding, alter airflow dynamics instantly. When straw, mud, or oversized grains wedge into the wire mesh, they block the upward air jets. This creates dead zones on the deck. You must implement a realistic maintenance schedule to combat this. Clean the screens daily using appropriate brass wire brushes. Never strike the mesh with hard steel tools, as this distorts the wire profile and ruins the galvanized coating.
Wear parts require strict monitoring. Wire mesh thins out over time due to the abrasive nature of silica-rich paddy. Once the mesh distorts, airflow becomes turbulent, and separation fails. Furthermore, eccentric bearing lubrication is non-negotiable. Dry bearings alter the vibration stroke, causing erratic deck movement. Grease these bearings according to the manufacturer's exact hour-meter recommendations, typically every 500 operating hours.
Component
Inspection Interval
Replacement/Service Action
Wire Mesh Sieves
Daily
Clean with brass brush; replace if wire thinning exceeds 20%.
Rubber Squeeze Valves
Monthly
Check for brittle edges or failure to seal; replace every 6 months.
Eccentric Bearings
Weekly
Apply high-temperature lithium grease; replace every 2000 hours.
Aspiration Channels
Weekly
Clear dust buildup to maintain -150 Pa static pressure.
Vibration Mounts/Springs
Quarterly
Inspect for cracks or sagging; replace as a complete set to maintain level.
Retrofitting and Structural Modifications
Operators must decide when to modify existing equipment and when to replace it entirely. If your current unit suffers from low stone removal efficiency, investigate structural retrofits first. Expanding air channels can eliminate bottlenecked airflow. Upgrading older eccentric drives to VFD-controlled motors provides modern adjustability without the capital expense of a new machine.
Retrofitting has limits. If the internal chassis is warped, or if the deck surface area is fundamentally too small for your current production volume, modifications will fail. When structural fatigue compromises the airtight integrity of the chamber, purchasing a new unit becomes the only viable operational decision. Welding patches onto a vibrating chassis rarely holds up under continuous industrial use.
Environmental Factors and Dust Extraction
Ambient conditions directly impact aerodynamic properties inside the separation chamber. High ambient humidity causes dust to clump and stick to the aspiration channels, restricting airflow. Dry, static-heavy environments cause light chaff to cling to the screens. You must make seasonal or even daily micro-adjustments to the air dampers to compensate for these environmental shifts.
Inadequate dust extraction exacerbates these problems. If your central baghouse is full or the fan belts are slipping, the destoner cannot pull enough negative pressure. The machine will choke on its own dust. Ensure your central aspiration system maintains a constant static pressure to support the destoner's requirements. Check the ductwork for leaks and ensure the rotary airlocks on the dust collector discharge properly.
Conclusion
Conduct a baseline yield-loss audit by measuring the exact percentage of good rice currently discharging in your stone reject chute over a standard production shift.
Inspect all internal sieves for wire thinning, mesh distortion, and blinding, replacing any damaged screens immediately to restore proper fluidization.
Check all aspiration channels and central dust collection lines for blockages that restrict upward airflow and cause pressure drops.
Install variable frequency drives (VFDs) on existing vibratory motors to allow operators to adjust stroke frequency on the fly based on paddy moisture.
Consult with process engineers to verify that your upstream feeding equipment delivers a uniform, surge-free material bed to the deck.
FAQ
Q: How do you adjust the airflow on a rice destoner?
A: You adjust airflow by manipulating the suction or blower dampers. Observe the grain bed through the inspection window; it should bubble gently like boiling water. If the bed is flat, open the dampers to increase fluidization. If good rice blows into the stone discharge, close the dampers slightly to reduce pressure.
Q: What causes good rice to come out with the stones?
A: Good rice discharges with stones primarily due to excessive airflow pushing the lighter grain up the incline. It can also occur if the deck inclination is too flat, or if you are overfeeding the machine, which disrupts the fluidized bed and forces mixed material into the reject chute.
Q: What is the ideal screen inclination angle for a destoner?
A: The ideal screen inclination typically ranges between 5 to 9 degrees. The exact angle depends on the grain type, moisture content, and targeted throughput. Steeper angles increase capacity but require higher vibration and air pressure, while flatter angles provide cleaner separation at lower capacities.
Q: How often should destoner screens be replaced?
A: Replace screens when you observe wear indicators such as wire thinning, mesh distortion, or localized blinding that cannot be cleaned. A sudden drop in separation purity or uneven fluidization often indicates that the screen profile is compromised and requires immediate replacement.
Q: What is the difference between a standalone destoner and a combined cleaner and destoner?
A: A standalone unit focuses entirely on density-based separation of heavy impurities. A combined unit integrates pre-cleaning scalper screens to remove large straw and fine sand before the material reaches the density-separation deck, consolidating two processes into a single vertical chassis to save floor space.
Q: Why is my paddy vibration cleaner leaving stones in the clean grain?
A: Stones remain in the clean grain due to inadequate airflow failing to lift the rice, allowing stones to flow downward. Other causes include blocked air channels, an excessively steep deck slope, or worn eccentric bearings that fail to provide the mechanical stroke needed to push stones upward.
Q: What is the purpose of rubber squeeze valves on a destoner?
A: Rubber squeeze valves discharge heavy impurities while sealing the separation chamber. They open under the weight of accumulated stones to eject debris and immediately close via negative pressure. This prevents ambient air leaks that would disrupt the internal fluidized bed and destroy separation accuracy.