Removing the outer bran layer to achieve market-grade whiteness without breaking the fragile endosperm is a constant battle in rice processing. Inefficient bran extraction and poor heat dissipation lead directly to uneven whitening, high percentages of broken rice, and rapid machinery wear. These failures threaten your milling yield and overall facility profitability. You need precise mechanical action paired with engineered pneumatic control to fix this. Integrated airflow and aspiration systems inside a modern rice whitener do much more than collect dust. They actively manage the milling environment. This technical guide evaluates how to select equipment capable of precise bran conveyance and optimal grain cooling. We will look at specific airflow metrics, roller configurations, and aspiration setups to help you maximize head rice yields on the floor.
Airflow Dictates Yield: Integrated aspiration systems do more than remove dust; they actively cool grains via jet streams, reducing thermal breakage and preserving head rice yield.
Configuration Matters: The choice between a vertical rice whitener and a horizontal unit fundamentally alters how gravity and airflow interact to clear bran from the milling chamber.
Roller Type Influences Air Requirements: An emery roller rice whitener (abrasive) and an iron roller (friction) generate different levels of heat and bran consistency, requiring specific ventilation slot and blower configurations.
System Integration is Critical: Standalone machine specs are insufficient; the whitener's airlock and aspiration capabilities must align with the facility's overall pneumatic infrastructure to prevent bran re-adhesion and rancidity.
The Mechanics of Bran Removal in a Rice Whitener
Defining the baseline for successful whitening requires strict metric tracking on the milling floor. Achieving uniform color and texture necessitates maintaining a less than 1-2% increase in broken grains per pass. Facility operators measure this metric continuously from the discharge hopper to ensure profitability. The bran layer removed from brown rice features a highly complex biological structure. It consists of the pericarp, seed coat, nucellus, and the aleurone layer. This outer profile is rich in fiber, vitamins, minerals, and natural oils. The oil content in the bran typically ranges from 15% to 20%. This nutrient-dense, oily composition presents a significant mechanical challenge during processing. It causes rapid rancidity and severe machinery clogging if not swiftly evacuated by targeted airflow.
Understanding the distinct dynamics of abrasive and friction milling helps you configure your pneumatic systems correctly. An emery roller rice whitener utilizes abrasive action. Sharp emery particles, usually bonded with resin or ceramic materials, physically cut the bran away from the endosperm. This cutting action generates fine, dry bran dust. The grit size of the emery roller dictates the size of the bran particles. Coarser grits remove material faster but require higher air velocity to suspend the larger dust particles in the exhaust stream.
Conversely, an iron roller relies on friction action. It forces the grains to rub against each other, against the steel milling screen, and against the resistance plates. The iron roller applies significantly greater pressure to the grain bed to strip the remaining bran layers. This intense mechanical pressure necessitates massive airflow to mitigate the resulting friction-induced heat. Softer grain textures, such as short-grain or newly harvested paddy, remain particularly vulnerable during these high-pressure processes. They suffer from severe thermal damage and over-peeling without adequate cooling mechanisms.
Friction causes rapid and dangerous temperature spikes within the tightly packed grain bed. Heat triggers immediate chemical consequences on the bran layer. Natural oils release from the aleurone layer upon heating. This extruded oil turns the loose bran dust into a sticky, dense paste. The paste rapidly blinds the 0.8mm to 1.2mm perforations in the steel milling screens. Screen clogging immediately halts the radial discharge of bran. This blockage leads to uneven whitening, severe heat accumulation, motor overload, and ultimately, massive grain fracture. You will see the main drive motor amperage spike just before the grain bed chokes.
How Airflow Systems Drive Even Bran Extraction
Modern milling equipment utilizes specific pneumatic mechanisms to control the internal chamber environment. High-pressure air is forced through a hollow main shaft. This air then exits through precisely engineered portholes or ventilation slots located along the milling cylinder. This internal-to-external airflow actively fluidizes the grain bed. Fluidization ensures uniform contact between the individual rice kernels and the abrasive surfaces. It prevents the grains from packing too tightly against the screens, which would otherwise cause localized pressure spikes and uneven milling.
External aspiration systems create continuous negative pressure within the milling chamber. This vacuum pulls the injected air, along with the detached bran particles, through the screen slots. The design of the aspiration hood determines how evenly this vacuum applies across the length of the screen. A poorly designed hood will pull heavily from the discharge end while leaving the feed end starved for air, resulting in uneven bran accumulation.
Airlock mechanisms play a vital role in this continuous process. They safely discharge the separated bran into collection silos or pneumatic conveying lines. They execute this transfer without breaking the vacuum required for continuous grain cooling. Proper airlock function maintains the static pressure gradient necessary for efficient bran evacuation. If the rubber wipers on a rotary airlock wear down, ambient air leaks into the system. This leak destroys the negative pressure in the milling chamber, instantly reducing the cooling capacity and allowing bran to build up on the screens.
Immediate bran conveyance prevents the fibrous, oil-rich material from adhering back to the polished grain. If bran lingers in the milling chamber, it smears across the warm rice surface. It also turns rancid within the machinery crevices, contaminating subsequent batches. High-velocity airflow ensures the bran moves instantly from the cutting zone to the discharge hopper. This continuous sweeping action keeps the screens clear and stabilizes the internal grain temperature.
To maintain this sweeping action, operators must monitor several pneumatic variables:
Main shaft air injection pressure.
Exhaust duct air velocity.
Static pressure at the aspiration hood.
Rotary airlock seal integrity.
Cyclone separator discharge efficiency.
Evaluating Equipment: Vertical Rice Whitener vs. Horizontal Configurations
Comparing structural designs requires evaluating airflow efficiency, footprint, and grain handling capabilities. The physical orientation of the milling chamber drastically changes how air and grain interact. Engineers design these machines to manipulate gravity alongside pneumatic forces to achieve the desired milling degree.
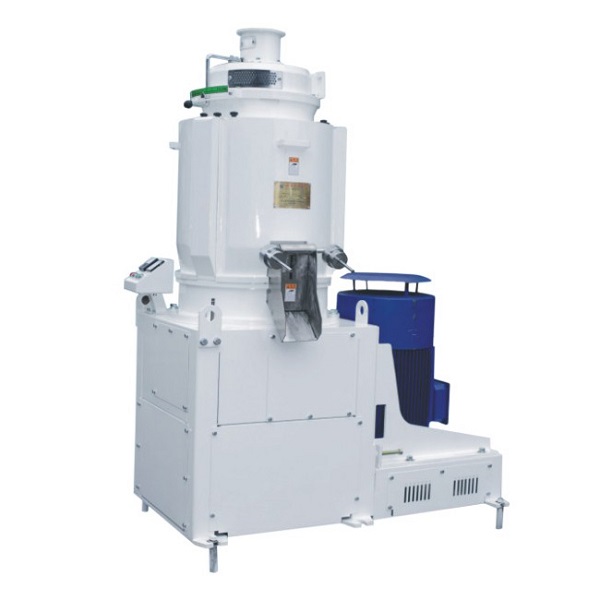
A vertical rice whitener utilizes gravity in tandem with upward or downward airflow to maintain a consistent grain density. The grain falls naturally through the annular space between the roller and the screen. This vertical drop ensures even pressure distribution across the entire circumference of the screen. Vertical units often achieve more uniform bran removal with lower static pressure requirements. This makes them particularly advantageous for processing soft grain textures that are easily damaged by uneven pressure gradients. The radial airflow in a vertical machine pushes bran outward 360 degrees, utilizing the entire screen area efficiently.
Horizontal machines present different airflow challenges. Gravity pulls the grain bed toward the bottom of the horizontal screen. This creates uneven grain distribution, often causing localized hot spots at the bottom and under-milling at the top. The bottom section of the screen wears out significantly faster than the top section. Horizontal setups require specific ventilation slot designs and powerful radiator fans to maintain cooling efficiency. Operators must carefully manage the feed rate and aspiration pressure to counteract the uneven settling of the grain bed. You often have to rotate the screens manually during maintenance to ensure even wear.
Evaluation Parameter
Vertical Configuration
Horizontal Configuration
Gravity Interaction
Promotes even grain density around the roller.
Causes grain to settle heavily at the bottom of the screen.
Airflow Distribution
Highly uniform radial discharge across 360 degrees.
Requires higher pressure to clear bottom screens; air favors top screens.
Screen Wear Pattern
Even wear across the entire cylinder.
Accelerated wear on the bottom half; requires manual rotation.
Footprint
Compact, utilizes vertical space efficiently.
Requires more floor space per unit.
Grain Suitability
Ideal for soft, easily broken grain varieties.
Effective for hard grains requiring high pressure and multiple passes.
Technical Evaluation Criteria for Rice Polishing Machines and Whiteners
Matching machine specifications to operational capacity determines the overall value of the investment. Buyers must evaluate the pneumatic requirements just as rigorously as the motor horsepower. Blower capacity and static pressure requirements dictate the success of the aspiration system. The ideal cubic feet per minute (CFM) and static pressure metrics scale directly with the machine's capacity. Standard 4S models processing 2.5 to 3 tons per hour require different blower sizing than high-capacity 6S production lines.
For a standard 3 to 4 ton-per-hour unit, you generally need an exhaust volume of 2000 to 2500 CFM. The static pressure at the machine's exhaust port should read between -100 and -150 mmH2O. Excessive airflow can dry out grains prematurely, causing stress cracks that lead to breakage in downstream equipment. Insufficient airflow leads directly to screen clogging, thermal damage, and a rapid drop in head rice yield. You must size the centrifugal fans correctly to match the specific resistance of your ductwork and cyclone separators.
Screen design heavily impacts air permeability. Engineers utilize hexagonal, octagonal, or round screen geometries. Each shape offers a different ratio of open area for air and bran to escape. Hexagonal screens often provide excellent resistance to grain wedging while maintaining high airflow rates. The slot width usually ranges from 0.8mm to 1.2mm depending on the grain variety. Short-grain rice requires narrower slots to prevent the grain from wedging into the holes and snapping. Easily accessible ventilation slots are critical for routine cleaning. Maintenance teams must clear these slots regularly to maintain optimal airflow.
Transitioning from the primary whitener to the secondary rice polishing machine introduces new airflow dynamics. The primary whitener handles heavy bran removal and requires massive dry airflow. The secondary polisher focuses on final surface smoothing and micro-bran removal. Polishers often integrate water mist into the airflow through the hollow main shaft. This controlled moisture softens the residual bran, allowing the friction rollers to create a smooth, glossy finish.
The aspiration system in a polisher must handle this moisture without allowing wet bran to cake inside the exhaust pipes. The air velocity in the polisher's exhaust duct must remain high enough (typically above 18 m/s) to keep the damp bran suspended until it reaches the cyclone. If the velocity drops, the wet bran will settle in the ductwork, creating hard blockages that require manual chipping to remove.
Screen Type
Open Area Percentage
Airflow Resistance
Best Application
Round Hole (Punched)
Low (25-30%)
High
Heavy friction milling, hard grains.
Slotted (Vertical)
Medium (35-40%)
Medium
General purpose whitening, long grain.
Hexagonal Wire
High (45-50%)
Low
High-capacity abrasive milling, soft grains.
Implementation Risks and Mitigation in Bran Aspiration
High-airflow milling systems introduce specific operational realities and maintenance burdens. Facility managers must address these risks proactively to maintain continuous production. Clogging and screen blinding remain the most frequent causes of unplanned downtime. High moisture paddy, inadequate blower speed, and soft grain peeling all contribute to rapid screen blinding. Processing paddy with a moisture content above 14.5% significantly increases the risk of the bran oils binding the dust into a paste.
Mitigation strategies require active monitoring and strict operational discipline. Facilities should implement automated screen clearing mechanisms where possible. Routine static pressure monitoring alerts operators to screen blockages before heat damage occurs. A sudden drop in exhaust airflow indicates an immediate need for screen inspection. You should install U-tube manometers or digital pressure sensors directly on the exhaust hoods of every machine.
Pneumatic network imbalance poses a severe risk during equipment upgrades. Installing a high-capacity whitener into an undersized facility aspiration network chokes the new machine. The existing fans cannot pull the required CFM through the new, larger milling chamber. The ductwork diameter might be too small, causing excessive friction loss. Pre-installation audits of existing cyclone separators and dust collectors are mandatory. These audits ensure the downstream equipment can handle the increased bran volume and air velocity.
Maintenance of cooling components prevents catastrophic heat buildup. Operators must follow strict maintenance schedules for radiator fans, airlocks, and internal shaft portholes. Dust accumulation on fan blades reduces their aerodynamic efficiency and causes vibration. Worn airlock seals allow vacuum leaks, destroying the negative pressure inside the milling chamber. Blocked shaft portholes prevent the internal jet stream from fluidizing the grain bed.
Monitor static pressure gauges hourly to detect early signs of screen blinding.
Inspect airlock rubber seals weekly to prevent vacuum loss in the aspiration network.
Clean internal shaft portholes during every scheduled screen replacement.
Audit cyclone separator efficiency annually to ensure proper bran discharge.
Calibrate blower motor speeds to match the specific moisture content of the incoming paddy.
Check ductwork elbows monthly for damp bran accumulation.
Measure main drive motor amperage daily to establish a baseline for normal milling resistance.
Conclusion
Audit your existing facility ductwork and cyclone capacity before purchasing high-capacity milling equipment to prevent pneumatic bottlenecks.
Install static pressure gauges on all exhaust hoods to give operators real-time visibility into screen blinding and airflow drops.
Implement a strict weekly inspection schedule for rotary airlock seals to eliminate vacuum leaks that degrade cooling efficiency.
Request empirical data from manufacturers regarding broken rice percentages at specific capacities for your exact grain variety.
Schedule a pilot test using your specific paddy to validate the machine's airflow efficiency and bran evacuation under real-world conditions.
FAQ
Q: What is the function of aspiration in a rice whitener?
A: Aspiration systems cool the grain bed by pulling ambient air through the milling chamber. This continuous airflow reduces thermal breakage caused by friction. It also rapidly conveys the detached bran out of the chamber, preventing screen clogging and allowing for appropriate storage in external silos.
Q: How does an emery roller rice whitener use airflow differently than an iron roller?
A: Abrasive emery rollers generate fine, dry bran dust that requires steady airflow for swift evacuation. Friction-heavy iron rollers apply greater mechanical pressure, generating significantly higher heat. Consequently, iron rollers require intense, high-velocity cooling air to mitigate thermal damage and prevent the bran oils from creating a sticky paste.
Q: What causes uneven bran removal in rice milling?
A: Uneven bran removal stems primarily from clogged milling screens and inconsistent grain bed pressure. Soft grain textures peeling unevenly also contribute to the problem. Furthermore, poor airflow failing to properly fluidize the grains causes localized hot spots and uneven contact with the abrasive rollers.
Q: How do you prevent rice breakage during the whitening process?
A: Preventing breakage requires integrating jet stream air through the main shaft to lower the internal grain temperature. Operators also use multi-pass whitening systems. Distributing the milling process across several machines reduces the mechanical pressure and thermal stress applied to the grain during each individual pass.
Q: What is the difference between a rice whitener and a rice polishing machine?
A: Whiteners remove the bulk of the nutrient-dense bran layer using heavy abrasion or friction. Polishers operate downstream, using fine friction and often a controlled water mist. The polisher smooths the grain surface, removes residual micro-bran, and improves shelf life by preventing rancidity.
Q: Why is grain cooling important in a vertical rice whitener?
A: Grain cooling prevents thermal stress, which preserves the structural integrity of the fragile endosperm. Heat causes the grain to become brittle and fracture under pressure. Maintaining a low temperature directly increases the yield of unbroken, premium head rice, maximizing the facility's profitability.